T: +86-13758587081
E: longtaiyarn@sina.com
E: longtaiyarn@sina.com
Longtai Textile, Building 58, Yuwang Xincun, Datang Street, Zhuji City, Shaoxing City, Zhejiang Province, China.
Views: 0 Author: Site Editor Publish Time: 2026-09-14 Origin: Site


Sourcing textile raw materials carries inherent downstream production risks. Inconsistent yarn elasticity or poor covering execution can quickly lead to fabric rejection, expensive machine downtime, and wasted capital. Manufacturers simply cannot leave material integrity to chance. For B2B buyers and textile procurement managers, relying solely on a supplier’s printed spec sheet is insufficient. Validating true quality requires a structured, objective, and repeatable testing framework in your own laboratory or through third-party auditors. We must proactively identify weak spots before weaving begins. This guide details the definitive physical and performance tests required to evaluate rubber covered yarn batches accurately. You will discover exactly how to measure tensile strength, verify wrap uniformity, and assess stretch recovery. We ensure these materials meet strict production tolerances before you ever scale up to bulk orders.
Unverified yarn directly threatens your entire production line. Uneven elasticity inevitably leads to uneven dyeing patches across large fabric rolls. Fabric warping frequently occurs during final finishing processes when yarns react unpredictably to heat. Ultimately, end-product failures like sagging activewear or snapped elastic bands will quickly destroy consumer trust. You incur massive financial losses when defective garments face mass rejection by retailers. By implementing strict physical testing, you catch these fatal flaws before the yarn ever touches a loom.
Procurement teams often fall into a dangerous trap regarding sample approvals. A highly successful initial sample never guarantees bulk order consistency. Suppliers frequently optimize small lab samples under perfect conditions. Bulk manufacturing runs face completely different mechanical stresses and environmental variables. Variables like machine tension, ambient humidity, and operator fatigue constantly shift. You must test random cones from actual bulk shipments to verify true statistical consistency.
We must establish strict baseline acceptable tolerances immediately. Your engineering team needs definitive limits for tension variations, weight fluctuations, and elasticity drop-offs. You establish these rules before integrating the material into high-speed weaving or knitting machines. Setting firm criteria allows quality assurance teams to accept or reject shipments objectively. It removes guesswork from the receiving dock and protects your downstream manufacturing efficiency.
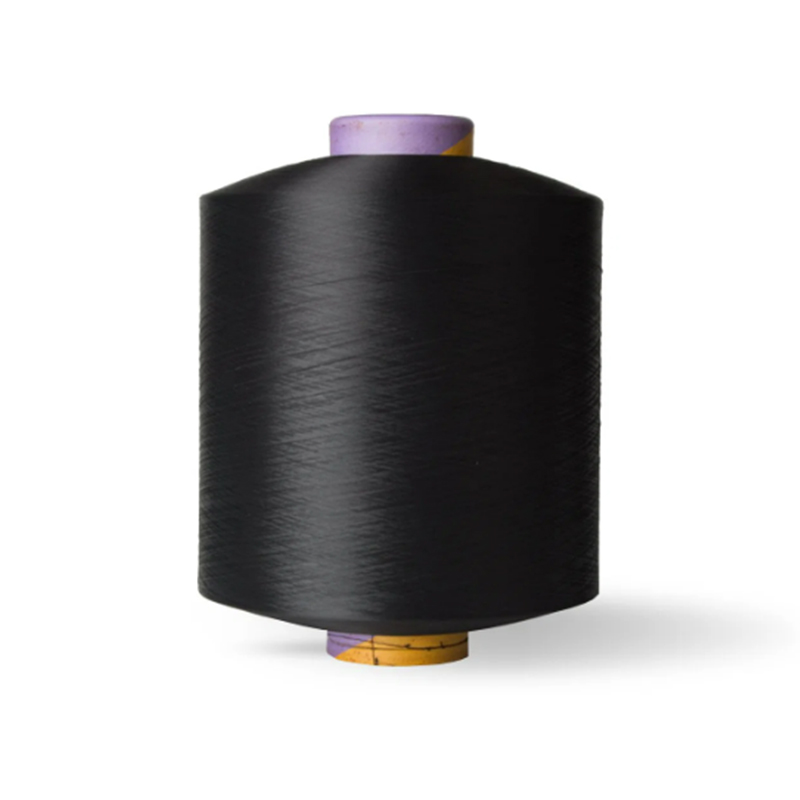
Modern textile production applies extreme stress to raw materials. We utilize standard tensile testing machines, such as Uster or Instron testers, to measure this exact breaking threshold. The machine grips the yarn and pulls it apart steadily. It records the precise force required to break the structural bond. High tensile strength ensures the material withstands intense loom tension without snapping. Unplanned yarn breaks halt production lines and require costly manual intervention.
Stretch recovery dictates how garments perform during actual human movement. Testers measure the yarn's ability to snap back to its original length after sustained stretching. Wearable textiles like athletic leggings and medical compression garments rely entirely on this metric. If a yarn stretches but fails to recover completely, the resulting fabric will bag at the knees or waist. We calculate the recovery percentage to predict long-term garment durability accurately.
The draft ratio represents the exact extension of the core during the wrapping process. Manufacturers stretch the core polymer before applying the outer protective sheath. Calculating this exact ratio prevents premature material fatigue. Incorrect drafting compromises both elasticity and lifespan. Over-drafted cores become brittle and break under minimal strain. Under-drafted cores yield bulky, inefficient yarns. You must follow a structured verification process to assess this:
Yarn count defines the specific thickness and weight profile of your raw material. Operators use standardized wrap reels to collect precise lengths of yarn under controlled tension. They then weigh these samples on precision analytical balances. This determines the exact weight per standardized length. Fluctuations in denier or tex strongly indicate poor manufacturing control at the supplier level. Uneven yarn counts inevitably produce streaky, defective knitted fabrics.
The outer filament must entirely conceal the inner elastic core. Technicians conduct intense visual and microscopic checks across random sample sections. They look for core exposure, an industry defect commonly called "grinning." When grinning occurs, the core catches on machinery or breaks during dyeing. Additionally, we must assess the twist level, measured in twists per inch (TPI) or twists per meter (TPM). Proper twist levels guarantee the outer wrapping will not unravel under mechanical stress.
Heat exposure radically alters material dimensions. Testers routinely subject yarn samples to boiling water or dry heat cabinets. This process measures absolute dimensional stability prior to the intensive dyeing and finishing phases. If the shrinkage rate exceeds your predetermined tolerance, the final knitted garment will warp uncontrollably during consumer washing. Identifying shrinkage characteristics early allows pattern makers to adjust their cut files accordingly.
| Testing Category | Primary Equipment | Standard Methodology | General Acceptance Limit |
|---|---|---|---|
| Tensile Strength | Tensile Testing Machine | ASTM D2256 / ISO 2062 | CV% < 5% |
| Yarn Count Accuracy | Wrap Reel & Analytical Scale | ASTM D1907 | ± 3% to ± 5% |
| Twist (TPI/TPM) | Twist Tester | ASTM D1422 | ± 5% from target |
| Boiling Water Shrinkage | Heated Water Bath | ASTM D2259 | Application dependent (typically < 3%) |
Structural differences dictate our evaluation frameworks. Traditional mechanical wrapping physically spirals an outer filament around the core. This requires testing specific twist integrity. Conversely, air entanglement uses high-pressure air jets to intermingle the outer fibers with the core. This modern method creates a softer, more integrated structure. You cannot test air-entangled products using traditional twist-measuring devices. The evaluation paradigm must shift entirely toward node stability and entanglement density.
Air-covered variants rely on physical entanglement nodes rather than continuous spiral twists. Testers specifically evaluate the frequency and stability of these air interlacing nodes. You must pull the yarn under simulated knitting tension to observe node slippage. If the interlacing nodes slip or untangle under tension, the outer sheath will separate from the core. This separation causes immediate machinery jams. Consistent nodal fastness ensures smooth runnability on high-speed circular knitting machines.
Testing rigor must always match the end-use application. Medical compression garments require extreme precision regarding stretch recovery and pressure consistency. Testers subject these yarns to thousands of cyclic stretch repetitions. Standard hosiery, however, prioritizes sheer visual uniformity and softness over heavy structural durability. You must customize your internal testing parameters based on the final product. Misaligning your testing rigor wastes time and artificially inflates procurement costs.
A trustworthy supplier operates with complete data transparency. They proactively share internal QA test results alongside every shipment. You should request technical data sheets detailing breaking strength limits, elongation boundaries, and specific count tolerances. If a supplier hesitates to provide detailed Certificates of Analysis (COAs), you should immediately disqualify them. Transparency proves they maintain strict internal control over their production variables.
High-quality data requires high-quality testing instruments. Verify whether the supplier actually uses industry-standard testing equipment like Uster evenness testers or calibrated tensile machines. Ask them for their equipment calibration schedules. Furthermore, ensure their testing methodologies align with recognized international standards like ASTM or ISO. A supplier utilizing uncalibrated, outdated equipment cannot guarantee the micro-tolerances required for modern textile manufacturing.
Procurement teams must remain highly skeptical during initial negotiations. Watch closely for the following critical warning signs:
Always mandate a pre-shipment sample pulled directly from the actual production run. Never settle for a carefully curated lab sample designed to impress. Once you receive the production sample, conduct your own in-house validation. If you lack the necessary laboratory equipment, hire a certified third-party testing agency. You secure the bulk order contract only after these independent tests confirm the supplier's initial claims.
Build a standardized internal testing checklist based strictly on the metrics discussed above. Document exact baseline tolerances for count, elongation, recovery, and twist. Hold your supply chain partners accountable to these specific technical thresholds before you ever finalize a long-term procurement contract. Taking these proactive steps ensures seamless production runs and protects your final brand reputation in the consumer market.
A: Yarn count is tested by winding a specific length of yarn on a standard wrap reel under controlled tension, then weighing it on a precision scale to calculate its Denier or Tex, factoring in the standard moisture regain. This ensures the material meets your specified thickness profiles.
A: Bare rubber yarn testing focuses purely on raw polymer elasticity and degradation limits. Covered yarn testing must simultaneously evaluate the core's stretch, the outer sheath's strength, and the mechanical synergy (twist/wrap integrity) between the two. You are testing a composite structure rather than a single material.
A: While specific applications vary, industry standards generally look for a count tolerance of ±3% to ±5%, and a strict elongation consistency to prevent fabric puckering during downstream processing. Consult your supplier's exact technical data sheet (TDS) for product-specific baselines before establishing internal limits.