T: +86-13758587081
E: longtaiyarn@sina.com
E: longtaiyarn@sina.com
Longtai Textile, Building 58, Yuwang Xincun, Datang Street, Zhuji City, Shaoxing City, Zhejiang Province, China.
Views: 0 Author: Site Editor Publish Time: 2026-10-20 Origin: Site


Transitioning a textile prototype into a scalable production run is a critical hurdle for any sourcing manager or textile developer. You might approve a flawless physical sample, only to face disaster during bulk manufacturing. Selecting incorrect yarn specifications directly leads to compromised fabric performance. You will likely experience unexpected manufacturing downtime or inflated production costs. To avoid these costly missteps, you need a highly precise specification strategy. We offer an objective breakdown of how technical variables dictate end-product behavior. You will discover a clear, actionable framework for balancing quality, compliance, and budget. Let us explore exactly how parameters like count and spinning technique define your final fabric architecture.
We must establish a foundational metric for evaluating textile scalability. Choosing the correct yarn specification guarantees seamless integration into your production line. You need absolute compatibility across knitting or weaving machinery. Manufacturers rely heavily on machine gauge alignment. If your yarn diameter clashes against the machine gauge, you face immediate friction. Needles break, tension fluctuates, and defects multiply rapidly.
Let us briefly differentiate standardized measurement systems. Textile engineers use indirect systems, like English cotton count (Ne), for spun fibers. Higher Ne numbers indicate finer yarns. For example, a 40s Ne is much finer than a 10s Ne. Conversely, direct systems like Denier or Tex measure continuous filaments. Higher Denier means heavier, thicker yarn. You must speak the correct measurement language when communicating with mills.
Let us look at how physical features translate to end-user outcomes. Low count (coarser) specifications yield high durability. They provide robust structural integrity against abrasion. You typically select coarse materials for heavy-duty workwear or commercial upholstery. High count (finer) alternatives yield superior drape. They deliver exceptional softness against the skin. Designers require finer counts for lightweight apparel and high-density technical fabrics.
Best Practice: Always request a pilot run of 50 kilograms before approving bulk orders. This confirms gauge compatibility on the actual production machines.
Your ultimate success criteria depend on mathematical alignment. Ensure your specified polyester yarn count accurately matches the required fabric GSM (grams per square meter). You must achieve this target without demanding excessive machine tension adjustments. Over-tensioning compromises fiber integrity. It stretches the core fibers beyond recovery. It ultimately ruins the hand-feel and dimensional stability of the finished roll.
You have several primary spinning methods available. Each technique fundamentally alters the final product architecture. Let us analyze these primary categories to help you make informed sourcing decisions.
Evaluating ring spun yarn reveals specific advantages. The traditional spinning process tightly twists individual fibers together. This continuous twisting action produces high tensile strength. It also creates a premium, exceptionally soft hand-feel. However, you must accept certain operational trade-offs. Ring spinning demands higher manufacturing costs. It runs at slower production speeds compared to modern alternatives. We recommend this method for high-margin apparel and comfort-driven textiles where tactile quality is paramount.
Evaluating Open-End (OE) spinning presents a distinctly different value proposition. The OE process utilizes high-speed rotors rather than spindles. It is highly uniform and incredibly cost-effective. Factories produce OE yarns at blistering speeds. The inherent trade-offs include lower tear strength. You will also notice a slightly harsher, stiffer hand-feel compared to ring-spun options. OE spinning serves as the optimal choice for budget-conscious projects. It excels in utility-grade applications like denim filler or basic industrial backing.
Evaluating Air-Jet or Vortex spinning highlights modern technological advancement. This sophisticated method uses compressed air currents inside a nozzle. The air tightly wraps outer fibers around a parallel central core. You achieve exceptional resistance to pilling and abrasion. Yet, distinct trade-offs exist here too. Air-jet machinery requires high-quality, uniform raw fibers to function correctly. The process is strictly limited to certain medium-to-fine count ranges. It remains ideal for intense performance wear. Specifically, we suggest it for uniforms requiring frequent industrial laundering.
Spinning Method Comparison Chart
| Spinning Method | Production Speed | Tensile Strength | Pilling Resistance | Best End-Use Application |
|---|---|---|---|---|
| Ring Spun | Slow | Very High | Moderate | Premium Apparel, Luxury Bedding |
| Open-End (OE) | Very Fast | Low to Moderate | Moderate | Utility Fabrics, Budget Workwear |
| Air-Jet / Vortex | Fast | Moderate to High | Excellent | Performance Wear, Uniforms |
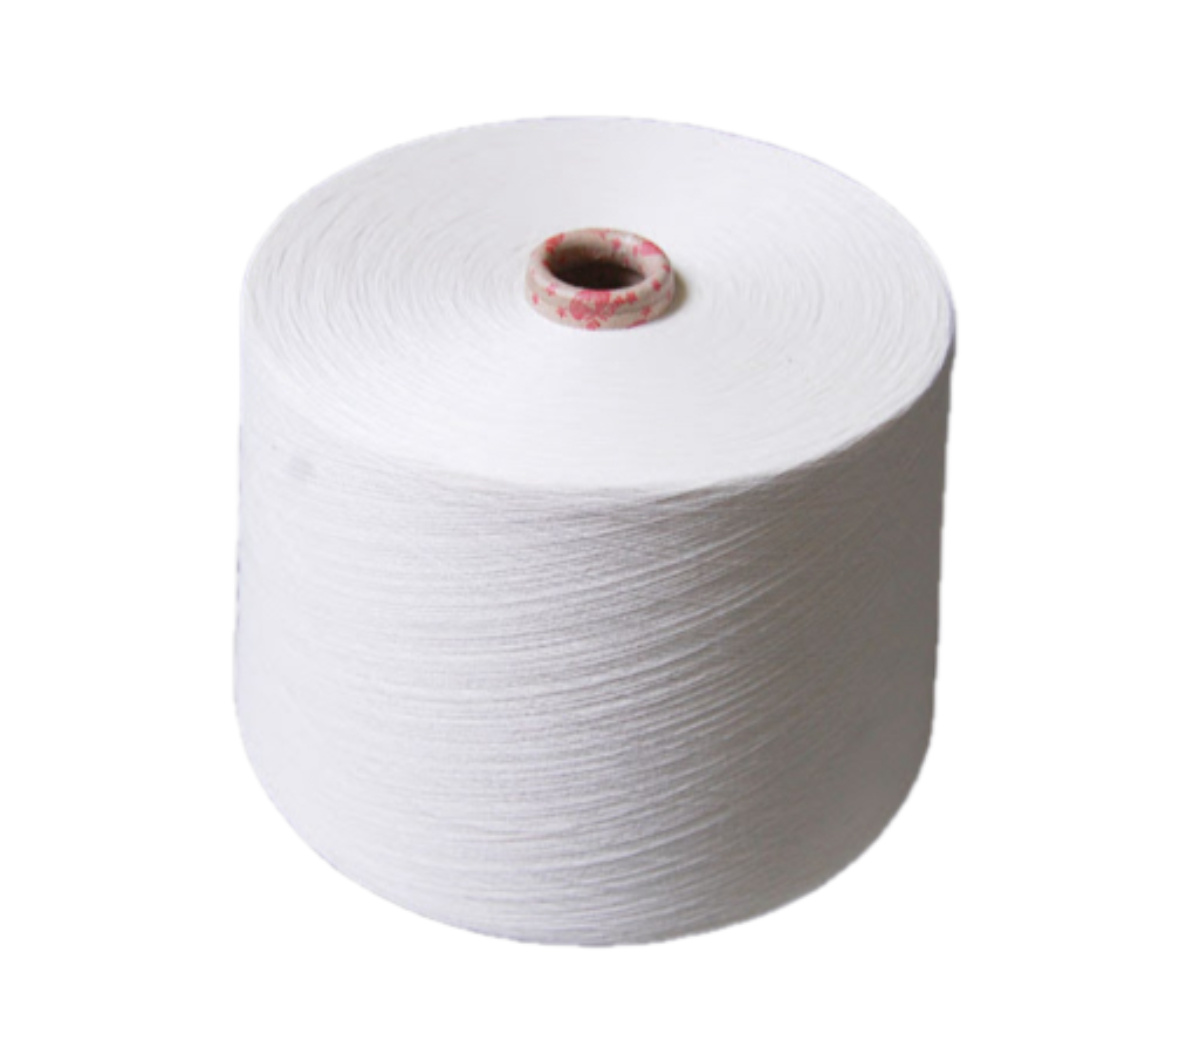
Now we map these technical specifications to tangible end-user outcomes. Durability and tensile strength depend on much more than raw material purity alone. The twist multiplier (TM) plays a crucial, often overlooked role. The chosen spinning method directly dictates both burst and tear strength. A higher twist level tightly binds fibers together. This friction prevents fiber slippage under intense physical stress. Standardized tests, like ISO 13934 for tensile strength, clearly reveal these mechanical differences.
Consider pilling resistance and overall surface integrity. An inherent trade-off exists between luxurious softness and surface resilience. Lower twist levels naturally create a softer hand-feel. However, these loose surface fibers easily pill during repetitive friction. Higher twist levels lock fibers down aggressively. Methods like air-jet spinning maximize surface resilience by wrapping stray hairs. They prevent fuzz formation entirely but feel slightly firmer against the skin.
Common Mistake: Specifying an ultra-low twist for maximum softness in activewear. The garment will pill aggressively after a single wash cycle.
Dye affinity and moisture management also require careful attention. The structural compactness of spun polyester yarn heavily impacts dye penetration. Highly compacted fibers resist dye liquor uptake inside the vat. They require adjusted dyeing profiles, higher temperatures, or extended hold times. Structural density also influences the application of topical chemical finishes. If you apply Durable Water Repellent (DWR) or wicking agents, yarn compactness matters deeply. Open structures absorb these liquid agents more readily into the core. Tighter structures keep the chemistry primarily on the outer surface. You must calibrate your mill's finishing processes accordingly to ensure durability.
You face real-world challenges on the factory floor every day. Inconsistent lots cause major operational headaches. We call this visual defect the Barré effect. It happens when you rely on cheaper suppliers lacking strict quality control. They often provide materials with poor Uster statistics. Uster stats measure critical parameters like unevenness (CV%), neps, and hairiness. When uneven material enters the knitting machine, it creates distinct horizontal banding in dyed fabrics. You cannot fix this expensive defect after dyeing. The entire fabric roll becomes second-grade merchandise.
Over-engineering your specifications introduces significant commercial risk. Do not pay for premium components unnecessarily. Sometimes an Open-End alternative perfectly meets all technical compliance requirements. It might also satisfy the aesthetic demands of your specific target market. You erode your profit margins quickly when you over-specify material grades. Always match the technical grade to the price point of the final consumer product.
Machine compatibility directly dictates overall factory efficiency. We measure this via Overall Equipment Effectiveness (OEE). High-speed manufacturing punishes incorrect twist levels ruthlessly. If you select the wrong specifications, you will suffer frequent breakages on the line. Every single breakage stops the machine entirely. Operators must manually rethread the system. This manual downtime destroys daily production schedules. You must precisely match the material strength to the machine's running tension.
You need a disciplined approach to source materials correctly. Follow this clear logic to select the right material for your upcoming production run.
Yarn specification remains a delicate commercial balancing act. It is never just a dry technical requirement. You must weigh aesthetic desires heavily against stark manufacturing realities. Building a tight, comprehensive specification sheet is your best defense against production failures. Document the precise count, acceptable variance limits, and exact spinning method required. This detailed document helps you maintain vital leverage in the supply chain. It guarantees structural consistency across multiple seasonal production cycles.
Take immediate action on your next textile development cycle. Prompt your suppliers for updated technical specification sheets today. Request physical sample cones for in-house machine tension testing. Solidify your technical foundation thoroughly before approving any bulk production runs.
A: Filament offers exceptionally high tenacity and a smooth, continuous surface. It is ideal for sleek performance wear and industrial uses. Spun versions consist of shorter staple fibers twisted together. This process mimics natural fibers, providing superior breathability, softer hand-feel, and better moisture management for everyday apparel.
A: You verify it in a controlled lab environment using a wrap reel and an analytical balance. The wrap reel measures a precise length of material. The balance weighs it accurately. By calculating the ratio of length to mass, you can confirm if the supplier claims match reality.
A: Not necessarily. While it is noticeably softer and stronger, it is significantly more expensive. It may not be required for items where extreme durability, utility, or low retail cost is the primary success metric. Open-end alternatives often suffice for budget-friendly casual wear.